OUR FACILITIES
Our flagship five-story facility spans a total floor space of 15,000 m², purpose-built to integrate our core operations under one roof. The building features a 3,000 m² state-of-the-art R&D centre, a 3,000 m² high-capacity warehouse, and a dedicated 3,000 m² production facility, ensuring seamless synergy from innovation to output.
R&D centre
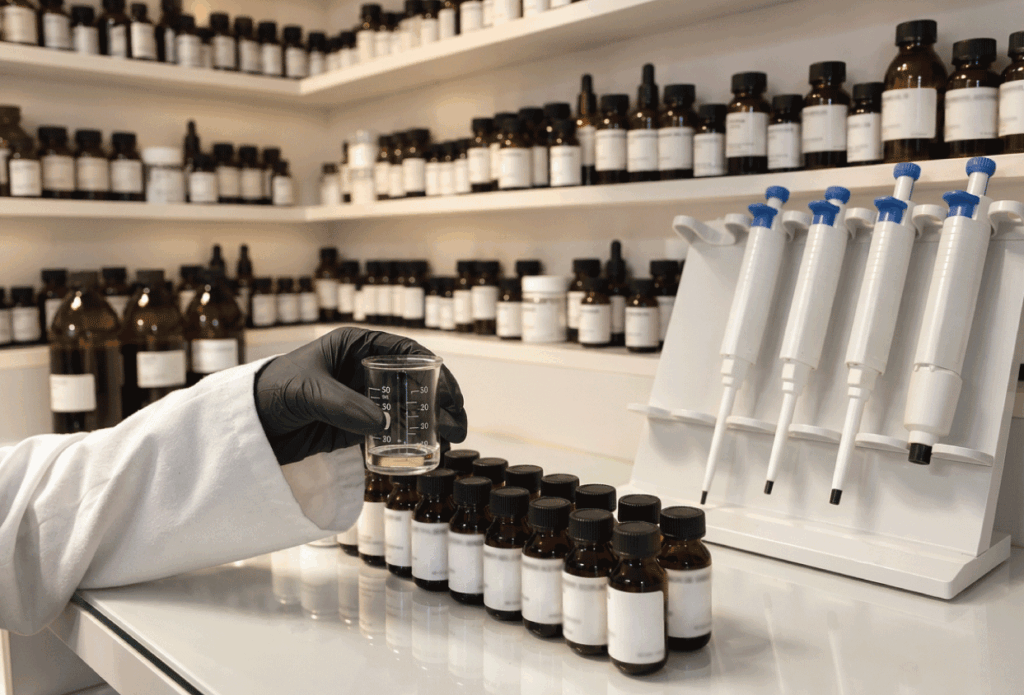
Our world-class infrastructure is equipped with advanced technical and analytical capabilities, including:
- Sensory Studio: A fully equipped testing space featuring modern sensory booths, bathroom pods, and dedicated laundry washing and drying facilities.
- Stability Testing Suite: Purpose-built environments supporting accelerated (48-hour), crash, and comprehensive long-term stability trials.
- Automated compounding: A robotic compounding system engineered for the high-precision formulation of standards.
- Next-Generation GC-MS Lab: Armed with 5 gas chromatographs, featuring Africa’s only Q-TOF instruments for unparalleled mass accuracy.
- Advanced Analytical Laboratories: A comprehensive testing suite housing 36 specialized pieces of analytical equipment for diverse testing methodologies
It also features advanced equipment such as:
- Gas Chromatography–Olfactometry (GC-O):
Sniffing ports connected to our GC-MS systems enabling analysts to correlate specific chromatographic peaks with actual perceived scent notes and off-smells
- Liquid Chromatography–Mass Spectrometer (LC-MS):
To study non-volatile, thermally labile, or high-molecular-weight ingredients that cannot pass safely through a standard gas chromatograph
- An electronic nose (e-nose) designed to mimic the mammalian sense of smell to rapidly detect, identify, and monitor complex odor profiles.
- Thermogravimetric and differential scanning calorimetry, which evaluates the physical stability, evaporation kinetics, and structural interactions of fragrances with their carriers or substrates, and allows us to do extensive evaporation studies
Warehouse
Our facility features a 3,000-square-meter main warehouse with a current inventory of 1,500 tons of materials, complemented by an overflow warehouse offering an additional 2,500 tons of capacity. To support diverse inventory needs, the facility is fully equipped with climate-controlled cold and hot rooms, alongside specialized areas dedicated to the storage of powdered raw materials.
Manufacturing facility
Our advanced production plant is engineered for maximum flexibility and accuracy, delivering a daily manufacturing capacity of 50 tons. The facility seamlessly scales from 5 kg pilot batches to 5-ton bulk tanks, utilizing software-driven processes to guarantee absolute precision. We are currently executing a phased automation roadmap to transition our semi-automated lines into fully robotic systems. Product integrity is maintained at every stage through rigorous pre-, in-line, and post-production quality control (QC) protocols.